In the fast-evolving landscape of food processing, achieving optimal hygiene and efficiency is essential. The introduction of Positive Drive Conveyors marks a significant advancement in this arena, combining innovative technology with hygienic design. These conveyors are designed to streamline operations while ensuring the highest safety and cleanliness standards. By minimizing the risks of contamination and enhancing product flow, Positive Drive Conveyors assist food processors in maintaining product integrity and meeting regulatory requirements effectively.
Understanding Positive Drive Conveyors
Positive drive conveyors utilize a unique operational mechanism that sets them apart from traditional conveyors. By employing a continuous belt that is positively engaged with the drive mechanism, they ensure a consistent and predictable motion. This feature significantly reduces slipping, which often leads to product misalignment and operational hiccups.
Key Benefits of Positive Drive Conveyors
- Enhanced Product Integrity: The precise control over movement prevents product damage during transportation.
- Improved Hygiene: With a design that minimizes area for contamination, these conveyors can be easily cleaned to maintain sanitary conditions.
- Versatile Applications: They are adept at handling a wide variety of products, from packaged goods to bulk materials.
The Importance of Hygiene in Food Processing
In a sector where safety is non-negotiable, hygiene takes precedence. Conveyors play a vital role in maintaining a clean environment that minimizes contamination risk. Positive drive conveyors, specifically, boast design features tailored to uphold stringent cleanliness standards.
How Positive Drive Conveyors Enhance Hygiene
The centerpiece of any reputable food processing facility is a system that promotes efficient sanitation practices.
- Seamless Cleaning: With smooth belt surfaces and tool-less disassembly, cleaning these systems is a straightforward task.
- Reduced Contamination Risks: Enclosed designs prevent the accumulation of dirt and allergens, making them preferable in sensitive environments.
- Corrosion-Resistant Materials: Many positive drive conveyors use stainless steel that meets food-safe standards, providing longevity and reliability.
Increasing Efficiency with Positive Drive Technology
While hygiene remains critical, efficiency is the lifeblood of successful food processing. The smart engineering of positive drive conveyors translates into remarkable throughput levels, making them indispensable in any production line.
Operational Advantages of Positive Drive Conveyors
By optimizing the flow of materials, these systems help eliminate bottlenecks and enhance productivity. Here’s how:
- Enhanced Speed Control: Their ability to precisely monitor and adjust speed contributes to improved workflow.
- Minimized Downtime: The robust construction and minimal need for maintenance result in less operational interruption.
- Energy Efficiency: With reduced energy consumption compared to other conveyor types, they contribute to lower operational costs.
Compliance and Regulatory Standards
In the world of food processing, compliance with regulations is paramount. Positive drive conveyors are designed with regulatory standards, such as those set by the FDA and USDA, in mind. Their compliance ensures that food safety is upheld without compromising production efficiency.
Features That Support Compliance
Implementing conveyors that align with industry standards provides food processors with peace of mind. Positive drive conveyors offer:
- Hygienic Design: Built to minimize harbour points that can harbor bacteria, these conveyors promote safe processing.
- Material Quality: Utilizing food-grade materials safeguards against chemical leach and contamination.
- Traceability: Systems that easily integrate with tracking technologies ensure compliance with supply chain standards.
Innovations and Future Trends in Positive Drive Conveyors
Positive Drive Conveyors are evolving with smart automation and digital monitoring. Sensors and IoT provide real-time data, enabling predictive maintenance and minimizing downtime.
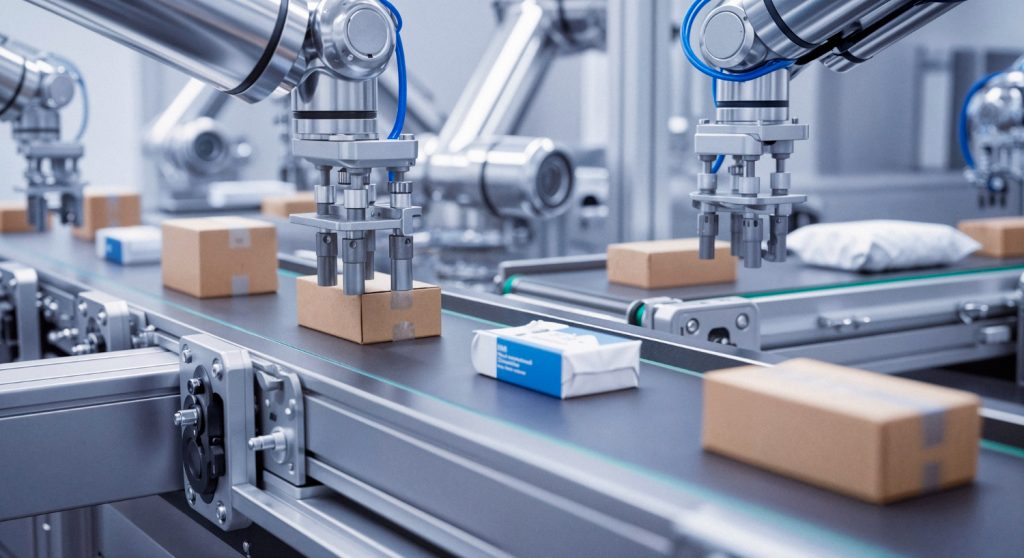
Integration with automated systems, like robotic arms and packaging lines, boosts efficiency and reduces manual handling, enhancing hygiene.
Energy-efficient motors and eco-friendly materials make these conveyors more sustainable, while modular designs allow easy upgrades and scalability.
In conclusion, positively driven conveyors represent a modern solution to age-old challenges in the food processing industry. By combining effective design with stringent sanitation measures, they provide a versatile, reliable, and compliant means for transporting products. Investing in such technology equips facilities not only with operational resilience but also with the confidence of adhering to high hygiene standards.
For more information on conveyor solutions in food processing, visit Cog-Veyor Systems.